Carbon Steel Buttweld Fittings Manufacturer and Supplier in India
Kalpataru Piping manufactures and supplies carbon steel buttweld fittings for process piping and pipeline applications across oil and gas, petrochemical, power generation, and construction industries. Our range includes seamless and welded elbows, tees, concentric and eccentric reducers, pipe caps, stub ends, and crosses, available in different sizes, wall thicknesses, and configurations to suit project requirements.
We offer fittings in ASTM A234 WPB for moderate- and elevated-temperature service, ASTM A420 WPL6 for low-temperature applications, and ASTM A860 WPHY grades for high-yield pipeline requirements. Manufactured using suitable hot-forming and cold-forming processes, our carbon steel buttweld fittings are produced according to applicable material and dimensional standards, including ASME B16.9 where relevant. Available options include different schedules and large-diameter fittings, subject to the material grade, fitting type, and size. Explore our range of carbon steel pipes and tubes for compatible piping requirements.
As a carbon steel buttweld fittings manufacturer and supplier in India, Kalpataru Piping supports project requirements with dimensional inspection, material test certificates, chemical composition verification, and mechanical testing as applicable. ISO 9001:2015 certification and IBR approval can be referenced where current and applicable to the supplied products. For competitive carbon steel buttweld fittings prices, contact our team with your required fitting type, material grade, size, schedule, quantity, and inspection requirements to request a quote.
Table of Contents
- What Are Carbon Steel Buttweld Fittings?
- Buttweld vs Socket Weld vs Forged Fittings
- Carbon Steel Buttweld Fittings Specifications
- Grades & Applicable Standards
- ASTM A234 WPB Chemical Composition & Mechanical Properties
- Dimension & Weight Reference
- Applications of Carbon Steel Buttweld Fittings
- Manufacturing Process & Quality Assurance
- Certifications & Documentation
- FAQ’s About Carbon Steel Buttweld Fittings
What Are Carbon Steel Buttweld Fittings?
Carbon steel buttweld fittings are pipe connection components designed to be welded directly to the pipe end-to-end (butt-to-butt), creating a flush, full-bore joint that is as strong as the pipe itself. Unlike socket weld or threaded fittings, buttweld fittings leave no internal crevice, making them ideal for high-pressure, high-temperature, and corrosive service lines where leak-tight integrity is non-negotiable.
The term “buttweld” refers to the welding method: the fitting’s beveled end is aligned with the pipe’s beveled end and fusion-welded around the full circumference. This results in a smooth, uninterrupted bore that minimizes turbulence, pressure drop, and the risk of solids deposition — all critical advantages in process piping systems.
At Kalpaturu Piping, our carbon steel buttweld fittings are manufactured from the same premium-grade carbon steel used in our carbon steel pipes and tubes, ensuring perfect metallurgical compatibility and uniform corrosion behaviour across the entire piping system. We also supply matching carbon steel flanges and carbon steel forged fittings so your procurement team can source a complete, compatible piping solution from a single, audited supplier.
- Buttweld vs Socket Weld vs Forged Fittings
- Specifications
- Chemical Composition & Mechanical Properties
- Grades & Applicable Standards
- Dimension & Weight Chart
- Carbon Steel vs Other Buttweld Fitting Materials
Buttweld vs Socket Weld vs Forged Fittings
|
Parameter |
Buttweld Fittings |
Socket Weld Fittings |
Forged Fittings |
|
Joint type |
Welded end-to-end; continuous bore |
Pipe inserted into a recessed socket, then fillet welded |
Threaded or socket-welded connection, depending on fitting type |
|
Typical size range |
Available across small- to large-bore sizes; often selected for medium- and large-bore process piping |
|
|
|
Internal flow |
Full-bore path with minimal internal obstruction |
Internal recess/crevice is present at the socket |
Depends on connection type |
|
Best suited for |
|
|
Compact, high-pressure connections |
Carbon Steel Buttweld Fittings Specifications
|
Parameter |
Recommended final detail |
|
Material Standard |
ASTM A234 / ASME SA234 Grade WPB. DIN and other legacy grades can be listed separately only where actually supplied. ASTM A105 should not be presented as a buttweld-fitting material grade. |
|
Low-Temperature Grades |
ASTM A420 WPL3, WPL6, WPL9, where offered |
|
High-Yield Grades |
ASTM A860 WPHY 42, WPHY 46, WPHY 52, WPHY 60, WPHY 65, WPHY 70 |
|
Dimension Standards |
ASME B16.9; ASME B16.28 for short-radius elbows/returns; ASME B16.25 for butt-welding end preparation; MSS SP-75 where applicable to high-strength WPHY fittings |
|
Size Range |
1/4″ NB to 48″ NB |
|
Wall Thickness |
SCH 5S, 10S, 20S, STD, 40S, 60, XS, 80, 100, 120, 140, 160, XXS |
|
Type |
Seamless, welded and fabricated |
|
End Finish |
Beveled ends to ASME B16.25. Other end preparations should be listed separately where specifically applicable. |
|
Testing |
Chemical analysis, mechanical testing, PMI, dimensional inspection and NDE/testing as required by the applicable specification or purchase order |
|
Certification |
EN 10204 3.1 / 3.2 Mill Test Certificate, IBR documentation and third-party inspection on request |
ASTM A234 WPB Chemical Composition & Mechanical Properties
Chemical Composition — ASTM A234 WPB (Max %)
Element |
Composition Requirement |
Carbon (C) |
0.30–0.35 max, as applicable |
Manganese (Mn) |
0.60–1.06, as applicable |
Phosphorus (P) |
0.035–0.050 max, as applicable |
Sulfur (S) |
0.040–0.058 max, as applicable |
Silicon (Si) |
0.10–0.35 or 0.10 min, subject to the applicable ASTM requirements and footnotes |
Chromium (Cr) |
0.30–0.40 max, as applicable |
Molybdenum (Mo) |
0.12–0.15 max, as applicable |
Nickel (Ni) |
0.40 max, where applicable |
Copper (Cu) |
0.40 max, where applicable |
Vanadium (V) |
0.08 max |
Mechanical Properties — ASTM A234 WPB
|
Property |
Recommended Final Detail |
|
Ultimate Tensile Strength, Min. |
60 ksi (415 MPa) |
|
0.2% Yield Strength, Min. |
35 ksi (240 MPa) |
|
Elongation, Min. |
Use the specimen-specific requirement of the applicable ASTM specification; do not publish one generic percentage |
|
Reduction of Area |
Remove unless specifically required and supported by the applicable ASTM specification or MTC |
|
Hardness, Max. |
Use the hardness limit specified by the applicable ASTM grade/specification; do not generalize 187 HBW or 197 HBW without confirmation |
Grades & Applicable Standards
Carbon Steel Grades
| Grade | Description |
| WPB | Standard service, most commonly used |
| WPBW | WPB fitting of welded construction; use the exact marking/heat-treatment terminology from the applicable ASTM edition and MTC. |
| WPHY 42 / 46 / 52 | High yield strength grades — pipeline service |
| WPHY 60 / 65 / 70 | Higher yield strength grades — high-pressure pipeline service |
Low-Temperature Grades
| Grade | Standard | Service Temperature |
| WPL3 | ASTM A420 | -150°F (-100°C) ASTM impact-test temperature; do not present as a blanket service-temperature guarantee |
| WPL6 | ASTM A420 |
50°F ASTM impact-test temperature: -50°F (-45°C) |
| WPL9 | ASTM A420 | -100°F (-75°C) ASTM impact-test temperature; do not present as a blanket service-temperature guarantee |
Applicable Standards
| Standard | Description |
| ASTM A234 | Material specification |
| ASME B16.9 | Factory-made wrought buttwelding fittings |
| ASME B16.28 | Short radius elbows and returns |
| MSS-SP-43 | Remove from the core WPB standards list unless a specific low-pressure corrosion-resistant fitting scope genuinely applies. |
| ASME B16.25 | Bevel end details |
| IBR | Indian Boiler Regulation Present under certification/regulatory compliance, not as a dimensional/material standard. |
Dimension & Weight Reference
A complete dimension and weight chart across all NPS 1/4″ to 48″ and every schedule is available on request. Sample values below for 90° long radius elbows:
|
NPS |
Outside Diameter (mm) |
90° LR Elbow — STD Weight (kg) |
90° LR Elbow — XH Weight (kg) |
|
1/2″ |
21.3 |
0.10 |
0.12 |
|
1″ |
33.4 |
0.20 |
0.26 |
|
2″ |
60.3 |
0.78 |
1.09 |
|
4″ |
114.3 |
4.00 |
5.71 |
|
6″ |
168.3 |
10.25 |
16.66 |
|
8″ |
219.1 |
21.10 |
32.16 |
|
12″ |
323.9 |
56.20 |
92.70 |
Carbon Steel vs Other Buttweld Fitting Materials
Choosing the right fitting material is a critical engineering decision. The table below helps project engineers and procurement teams compare carbon steel against the most common alternatives.
|
Property |
||||
|---|---|---|---|---|
|
Max. Service Temp. |
800 deg F (427 deg C) |
1200 deg F (649 deg C) |
1500 deg F (816 deg C) |
2000 deg F (1093 deg C) |
|
Min. Service Temp. |
-20 deg F (-29 deg C) |
-20 deg F (higher with WPL grade) |
-325 deg F (-198 deg C) |
Cryogenic capable |
|
Corrosion Resistance |
Moderate (carbon oxidises; needs coating) |
Moderate to good (Cr-Mo grades) |
Excellent (passivating oxide layer) |
Outstanding (chloride, acid, H2S) |
|
Tensile Strength |
60,000 psi (min) |
60,000-90,000 psi |
70,000 psi (min) |
100,000 psi (min) |
|
Weldability |
Excellent (standard carbon steel filler) |
Good (preheat required) |
Good (low-carbon grades preferred) |
Requires Hastelloy filler |
|
Relative Cost |
Baseline (1x) |
2.5-4x |
4-6x |
15-25x |
|
Best-Fit Service |
General process, oil & gas, water |
High-temp steam, refineries |
Corrosive chemicals, pharma, food |
Severe chloride, acid, HF |
|
Procurement Lead Time (Kalpaturu) |
3-5 days (stock) |
2-4 weeks |
1-2 weeks |
3-6 weeks |
Types of Carbon Steel Buttweld Fittings
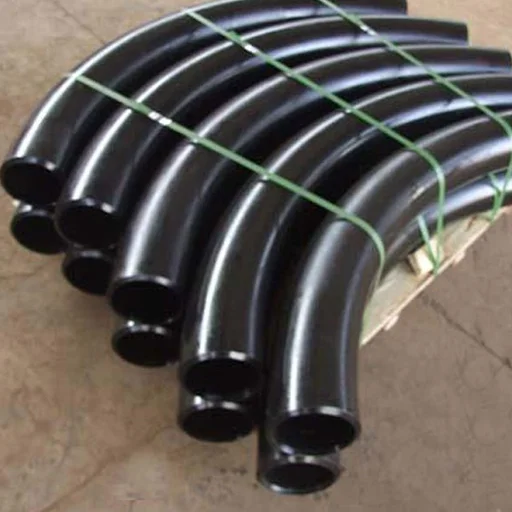
_Carbon Steel Bend
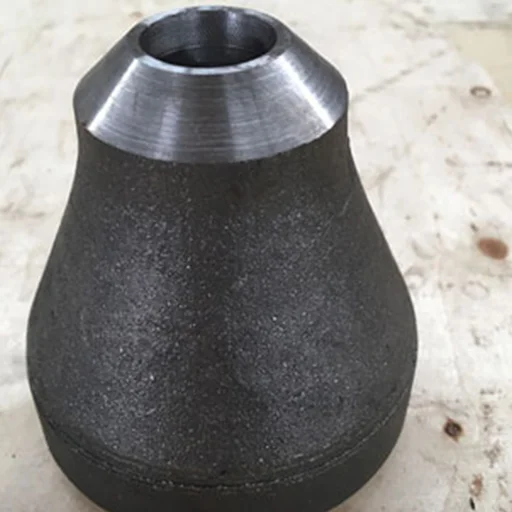
_Carbon Steel Concentric Reducer
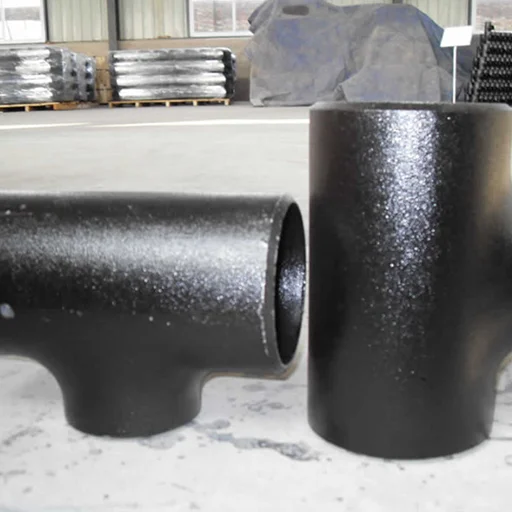
_Carbon Steel Equal Tee
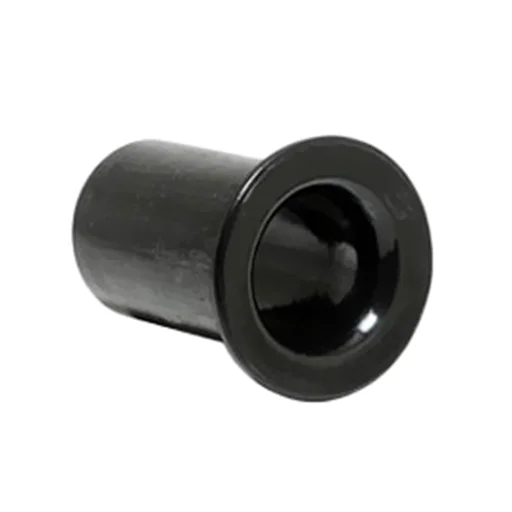
_Carbon Steel Long Stub End
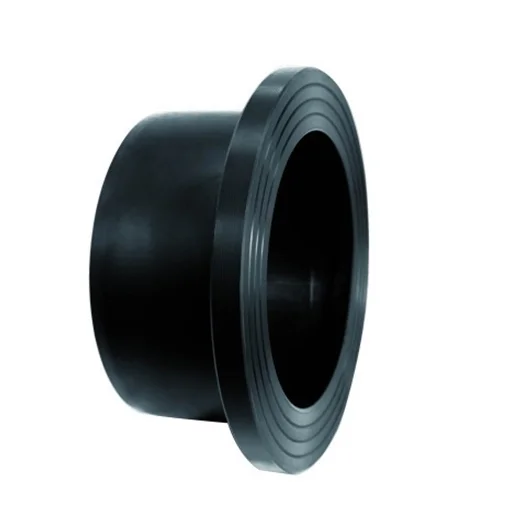
_Carbon Steel Short Stub End
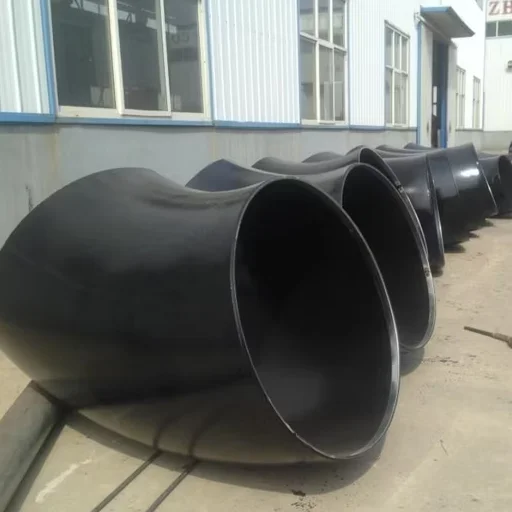
Carbon Steel 45 Degree Elbow
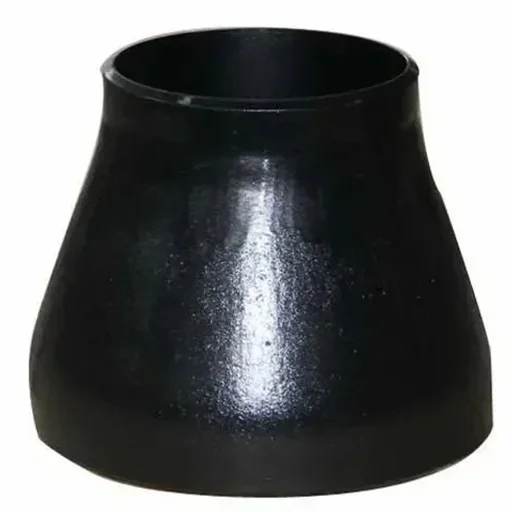
Carbon Steel Eccentric Reducer
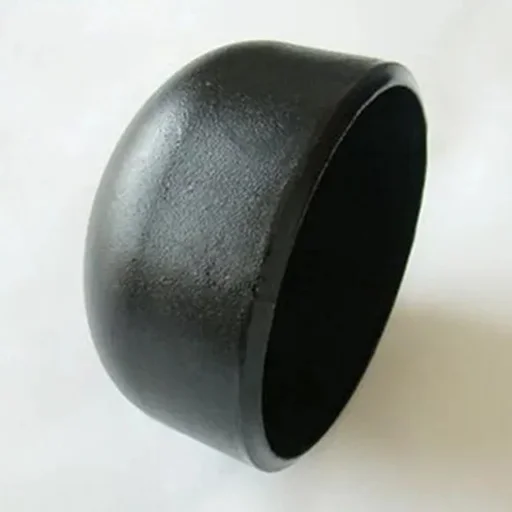
Carbon Steel End Cap
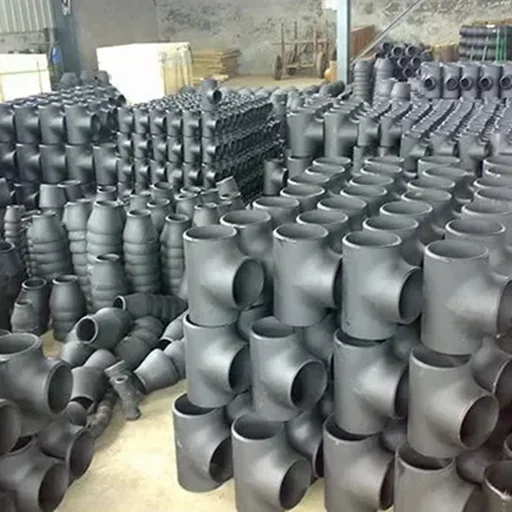
Carbon Steel Equal Cross
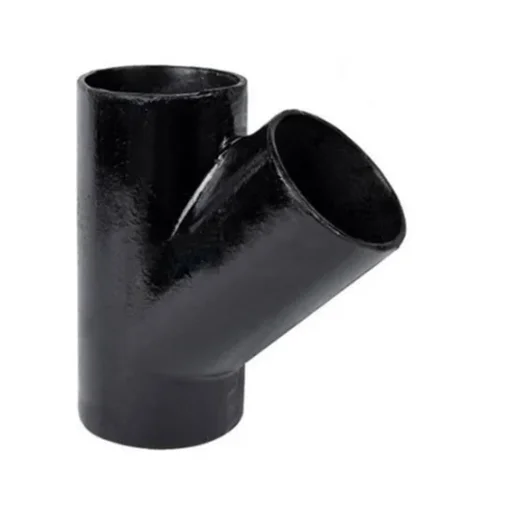
Carbon Steel Lateral Tee
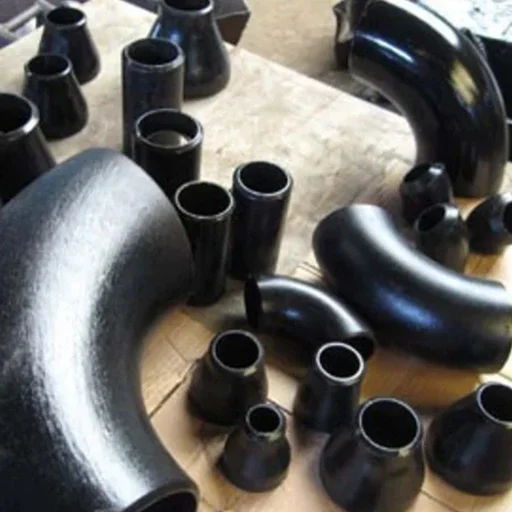
Carbon Steel Pipe Fittings
Carbon Steel Buttweld Fittings Applications
Carbon steel buttweld fittings are the backbone of industrial piping across virtually every heavy industry. Their combination of strength, weldability, and cost-effectiveness makes them the default specification on projects globally.
Oil & Gas (Upstream, Midstream & Downstream)
- Wellhead gathering lines and production manifolds
- Crude oil and gas transmission pipelines (WPHY grades for API 5L compatibility)
- Refinery process piping: crude distillation, hydrocracking, FCC units
- Offshore platform structural and process piping
Petrochemical & Chemical Processing
- Reactor feed and effluent lines at elevated temperatures
- Solvent and alkali transfer lines where carbon steel is acceptable
- Ethylene, propylene, and polymer plant piping systems
- Tank farm interconnecting pipework
Power Generation
- Steam and condensate return lines in thermal power stations
- Boiler feed water piping with IBR-compliant fittings
- Cooling water distribution headers
- Auxiliary piping for turbine lube oil and control fluid
LNG & Cryogenic Plants (A420 WPL6 Grade)
- Liquefied natural gas receiving terminals
- Cryogenic storage tank fill and discharge headers
- Cold-box piping for air separation units (down to -100 deg F / -73 deg C)
- Regasification plant piping
Infrastructure & Construction
- Fire suppression (sprinkler) system mains and headers
- Water supply and sewage treatment plant piping
- HVAC chilled water and heating system pipework
- Structural piping for shipbuilding and marine applications
High-Yield Pipeline Systems (A860 WPHY)
- Cross-country natural gas and crude oil trunklines
- Subsea pipeline spools requiring API 5L X52 to X70 material matching
- Deepwater riser base connections
For projects spanning multiple material families, pair your carbon steel buttweld fittings with our alloy steel buttweld fittings for high-temperature service or our stainless steel buttweld fittings for corrosive fluid service, all manufactured and documented to consistent quality standards.
Manufacturing Process & Quality Control
Quality in a buttweld fitting is not just about the finished dimensions — it starts with raw material selection and runs through every stage of forming, heat treatment, testing, and documentation. Here is how Kalpaturu Piping does it.
Stage 1: Raw Material Procurement We source mother pipes and plates from TATA Steel, SAIL, and other primary producers with full EN 10204 3.1 mill test reports. Each heat is checked against the applicable ASTM chemistry before entering production. Only material that passes our incoming quality control (IQC) inspection enters the manufacturing line.
Stage 2: Hot Forming & Cold Forming Elbows and tees up to 24” NPS are produced by hot-push forming (mandrel extrusion) over induction-heated seamless or welded pipe blanks. Reducers and caps are formed by hydraulic pressing of heated pipe sections. Cold-forming is used for thin-wall, small-bore fittings where tight dimensional tolerances are required. All forming operations preserve the nominal wall thickness within the tolerances of ASME B16.9.
Stage 3: Heat Treatment All hot-formed fittings are normalized (or normalized and tempered for WPC grade) to relieve forming stresses and restore the required mechanical properties. Heat treatment cycles are calibrated against NIST-traceable pyrometers and logged batch by batch.
Stage 4: Dimensional Inspection Every fitting is gauged against ASME B16.9 dimensional tables: center-to-end, end-to-end, wall thickness at crotch and intrados, and bevel angle per ASME B16.25. Our CMM and manual gauging records are retained for five years.
Stage 5: Non-Destructive Testing (NDT)
- Hydrostatic test: Applied per ASME B16.9 or client specification
- Radiographic Testing (RT): For welded fittings and on request
- Ultrasonic Testing (UT): Wall thickness verification and lamination check
- Dye Penetrant (PT) / Magnetic Particle (MT): Surface flaw detection on critical grades
- Positive Material Identification (PMI): 100% PMI available for all heats on request
Stage 6: Mechanical Testing Tensile test, yield strength test, hardness test (Brinell, max 197 HBW for WPB), Charpy V-notch impact test (mandatory for A420 WPL6 at test temperature), and bend test are performed on test rings cut from production pipe per heat.
Stage 7: Certifications & Third-Party Inspection
|
Certification / Approval |
Scope |
|---|---|
|
ISO 9001:2015 |
Quality management system |
|
IBR (Indian Boiler Regulations) |
Boiler and pressure vessel piping |
|
PED 2014/68/EU |
European pressure equipment directive |
|
ASME U Stamp (via TPI) |
Pressure vessel components |
|
TPI by Bureau Veritas / Lloyd’s / DNV |
Third-party inspection on request |
We supply with EN 10204 3.1 material test reports as standard. EN 10204 3.2 (TPI-witnessed) is available for all critical orders.
Why Choose Kalpaturu Piping for Carbon Steel Buttweld Fittings?
- One-Stop Carbon Steel Supply Procure your complete carbon steel system from a single audited source. Beyond buttweld fittings, Kalpaturu Piping supplies carbon steel flanges, forged fittings, pipes and tubes, round bars and wires, plates and sheets, and pipe spools — all traceable to the same heats and quality system.
- Broad Size and Schedule Range We hold finished stock in the most common sizes (1/2″ to 12″ NPS) and manufacture to order in sizes up to 48″ NPS and any schedule from SCH 5 to XXS. Short lead times on non-stock items thanks to our 5,000+ MT raw material inventory.
- Fully Documented Supply Chain Every order ships with EN 10204 3.1 MTRs, dimensional inspection reports, heat treatment records, and hydrostatic test certificates. NABL-accredited lab reports, TPI, and EN 10204 3.2 are available on request. Full traceability from raw material heat to finished fitting is our baseline, not an upgrade.
- Competitive Pricing with No Compromise on Quality Our integrated sourcing, in-house forming, and efficient logistics let us offer prices that are consistently 10–18% below import parity, without reducing material specification, testing, or documentation. We publish standard price lists quarterly and offer project-rate agreements for bulk orders.
- Fast Quote & Short Lead Times Standard inquiries receive a written quote within 24 hours. Stock items ship within 3 business days. Manufactured-to-order fittings are delivered in 3–6 weeks depending on size and quantity. Urgent requirements for carbon steel pipe spools can be fast-tracked.
- Global Export Experience We have exported carbon steel buttweld fittings to projects in the UAE, Saudi Arabia, Qatar, USA, UK, Germany, Singapore, Australia, and 40+ other countries. Our export documentation team handles SONCAP, COO, FORM E/A/D, and all other destination-country requirements seamlessly.
Frequently Asked Questions
What are Carbon Steel Buttweld Fittings?
Carbon Steel Buttweld Fittings are piping components used to connect, change direction, reduce pipe size, or terminate pipelines. They are welded directly to pipes to provide strong, leak-proof, and permanent connections.
What are Carbon Steel Buttweld Fittings used for?
Carbon Steel Buttweld Fittings are used in oil and gas, petrochemical, power generation, chemical processing, water treatment, and industrial piping systems that operate under high pressure and temperature.
What is the difference between Carbon Steel Buttweld Fittings and Forged Fittings?
Carbon Steel Buttweld Fittings are welded to pipes and are commonly used in larger pipe sizes, while Forged Fittings are threaded or socket welded and are typically used for smaller pipe sizes and high-pressure applications.
What schedules are available for Carbon Steel Buttweld Fittings?
Carbon Steel Buttweld Fittings are commonly available in Schedule 10, Schedule 20, Schedule 40, Schedule 80, Schedule 160, and XXS, depending on the pipe size and application requirements.
Are Carbon Steel Buttweld Fittings suitable for high-temperature applications?
Yes, Carbon Steel Buttweld Fittings are suitable for high-temperature and high-pressure applications when manufactured in appropriate grades such as ASTM A234 WPB and used within their specified operating limits.
Can Carbon Steel Buttweld Fittings be welded?
Yes, Carbon Steel Buttweld Fittings are specifically designed for butt welding, creating strong, durable, and leak-free joints in industrial piping systems.