What Is The Difference Between 304, 18-8 and 316 Stainless Steel?

What Is The Difference Between 304, 18-8 and 316 Stainless Steel?

When dealing with stainless steel, it becomes imperative to distinguish between the various grades, such as 18-8, 304, and 316, particularly in relation to their suitability for different applications. It’s essential to ensure that the chosen grade aligns with the demands of the intended working environment. Let’s delve into the nuances of these grades while keeping in mind that, fundamentally, both 18-8 and 304 share identical chemical compositions; their suitability depends on specific applications.

Understanding Grade 18-8/304 and Its Attributes

Both 18-8 stainless steel and 304 stainless steel exhibit the same chemical composition. The nomenclature “18-8” denotes their makeup, consisting of 18% chromium and 8% nickel. This cost-effective variant finds its niche in commercial food processing, refrigeration, and dishwashing applications due to its commendable resistance to corrosion. The 304 grade serves as a general-purpose grade, but there are two notable subgrades within this category. Firstly, the 304L, characterized by its low carbon content, can withstand moderately high temperatures. Secondly, the 304H, a high carbon grade, boasts exceptional tolerance for extreme temperatures.

It’s worth noting that machining the 304/18-8 grades often necessitates specialized tools compared to lower-grade stainless steel options.

18-8 Stainless Steel Advantages and Disadvantages

18-8 grade stainless steel has garnered acclaim for its remarkable resistance to corrosion. However, it does exhibit vulnerability to corrosion when exposed to chlorides, such as saltwater. Consequently, it may not be the optimal choice for applications in marine environments. On a positive note, 18-8 grade stainless steel boasts properties that allow for easy bending and shaping without compromising its overall strength and durability. This particular type of stainless steel is not only highly cost-effective but also demands minimal maintenance. Furthermore, it demonstrates an impressive yield strength.

Applications of 18-8 Stainless Steel

Within various industries, 18-8 grade stainless steel finds versatile applications. It is commonly employed in sectors such as wastewater treatment, restaurant and catering, medical, and transportation. However, it is worth noting that it is unsuitable for use in marine settings.

304 Stainless Steel Pros and Cons 

304 stainless steel offers a range of advantages that position it as a prominent choice within the realm of mild steels. Its notable strength sets it apart as a reliable material for diverse applications. Additionally, it exhibits commendable resistance to corrosion, making it an appealing option. When compared to its counterpart, 316 stainless steel, 304 stainless steel stands out as being more malleable and easier to shape. Nevertheless, it’s crucial to acknowledge that, similar to 18-8 grade stainless steel, 304 stainless steel is susceptible to corrosion when exposed to saline environments.

Applications of 304 Stainless Steel

The versatility of 304 stainless steel finds widespread application in the manufacturing of various products, including but not limited to sinks, pots, pans, and tables, among others. This material’s adaptability and durability render it a favored choice in industries such as dairy, food processing, and brewing.

316 Stainless Steel Advantages

The chemical composition of 316 stainless steel differs somewhat from that of 304. SS 316 comprises 16% chromium, 10% nickel, and trace amounts of other elements. Within the realm of 316 stainless steel, various iterations exist. For instance, there is the 316L, known for its low carbon content. Additionally, the 316F represents a free machining grade, while the 316N is a high nitrogen grade. These variants are particularly well-suited for marine environments or areas with elevated salinity levels.

One distinguishing feature of 316 stainless steel is its superior strength in comparison to 304 stainless steel. It offers exceptional resistance against corrosion, as previously mentioned, and provides protection against pitting and damage caused by caustic chemicals. These attributes make it a preferred choice for applications in refineries, chemical processing, and storage facilities, and it performs admirably in marine environments.

As always, it is crucial to meticulously select the appropriate product that aligns with the specific demands of the working environment. This selection process should factor in considerations of budget and intended application to ensure prolonged performance and structural integrity.
Brass Pipes: Advantages and Disadvantages

Brass Pipes: Advantages and Disadvantages

5 Advantages of Brass Pipes

Brass Pipes Durability:

Brass pipes offer an unparalleled advantage in terms of durability. Composed of an exceptionally strong metal, brass can withstand the ravages of corrosion, rust, and various environmental factors for extended periods without necessitating replacement or repair. Remarkably, it demands no specialized maintenance or care to retain its optimal condition. This characteristic renders it an exceptional choice for plumbing endeavors requiring longevity without the need for recurrent maintenance or repairs.

Brass Pipes Are Easy to Install:

Brass presents a visually pleasing aesthetic compared to alternative metals such as copper or steel. Its golden hue adds a touch of elegance and sophistication to any space or structure employing brass piping applications. Consequently, it emerges as the ideal selection for diverse settings, including residential homes, commercial edifices, and projects where aesthetics play a pivotal role.

Brass Pipes Easy to Customize:

Brass pipes are relatively easy to work with compared to other metals such as copper or steel. Their malleability allows for straightforward bending and shaping, making them ideal for customized piping applications that require specific forms and configurations.

Brass Pipes Are Fire Resistance:

Another noteworthy advantage of brass pipes is their resistance to fire. They exhibit slower ignition properties compared to alternative materials, providing an added safety feature. Furthermore, in the event of a fire, brass pipes do not contribute to the rapid spread of flames.

Brass Pipes Are Cost Effective:

Brass pipes provide a cost-effective solution in the long run. While they may come with a higher initial price tag due to their durability and visual appeal, their longevity and minimal maintenance requirements translate into cost savings over time.

5 Disadvantages of Brass Pipes

Brass Pipes Higher Initial Cost:

One notable disadvantage of brass pipes is their initial cost, which tends to be higher compared to materials like copper or steel. This price premium is attributed to the material’s durability and aesthetic appeal.

Brass Pipes Potential Lead Content:

Another concern with brass pipes is the potential presence of lead. Although the levels of lead in brass pipes are typically low, there is a risk of lead leaching into the water flowing through them, which can be harmful, especially to pregnant women and young children.

Brass Pipes Susceptibility to Corrosion:

Over time, brass pipes may corrode, leading to water contamination and leaks. Corrosion can result in water quality issues and potential damage to your property.

Brass Pipes May Be Noisy:

Brass pipes can generate noise as water flows through them, which may be disruptive and annoying. In certain situations, this noise can even disturb sleep if brass pipes are installed in a bedroom or nearby.

Brass Pipes May Require Special Maintenance:

Maintaining brass pipes may require extra effort to prevent corrosion and lead contamination. Periodic cleaning with specialized products may be necessary, and regular water testing might be recommended if brass pipes are part of your plumbing system.

In Conclusion:

In summary, brass pipes offer durability, aesthetics, and fire resistance, making them a solid choice for plumbing projects. However, their higher brass pipe price, potential lead content, susceptibility to corrosion, noise generation, and special maintenance requirements should be carefully considered. Ultimately, the decision to use brass pipes should align with your specific needs and budget, while also weighing the alternatives like copper or steel pipe systems.

Alloy 20 / UNS N08020

Alloy 20 / UNS N08020

Austenitic alloy – Alloy 20 is based on nickel, iron, and chromium and has high corrosion resistance in settings including sulfuric acid and other hostile fluids. This alloy is stabilized with niobium to stop intergranular corrosion. When carefully compared to higher nickel-based alloys, Alloy 20 may offer possible cost savings while outperforming regular stainless steels.

Alloy 20 Chemical Composition:

ElementContent (%)
Iron, Fe35
Nickel, Ni32-38
Chromium, Cr19-21
Copper, Cu3-4
Manganese, Mn≤2
Molybdenum, Mo2-3
Niobium, Nb≤1
Silicon, Si≤1
Carbon, C≤0.07
Phosphorous, P≤0.045
Sulfur, S≤0.035

Alloy 20 Physical Properties:

PropertiesMetricImperial
Density8.05 g/cm30.291 lb/in3

Alloy 20 Mechanical Properties:

PropertiesMetricImperial
Tensile strength (annealed)620 MPa89900 psi
Yield strength (annealed)300 MPa43500 psi
Elongation at break (annealed)41%41%

Nickel Alloy 20 Thermal Properties:

PropertiesMetricImperial
Thermal expansion co-efficient (@20-100°C/68-212°F)14.7 µm/m°C8.17 µin/in°F
Thermal conductivity12.3 W/mK85.4 BTU.in/hrft².°F

Industries and Applications:

Alloy 20 distinctive attributes find resonance in a multitude of industries. From chemical processing to pharmaceuticals, this alloy proves its mettle in various applications. We unravel the sectors that have harnessed the power of Alloy 20 and delve into specific use cases that highlight its adaptability and reliability.

Resistance to Corrosion:

One of Alloy 20 most remarkable features is its unparalleled resistance to corrosion. Delving into the alloy’s molecular structure, we uncover the mechanisms that empower Alloy 20 to withstand the harsh environments of chemical compounds, particularly those containing sulfuric acid. Through real-world examples and scientific insights, we illustrate how Alloy 20 stands as a stalwart guardian against the corrosive forces that can compromise other materials.

Fabrication and Heat Treatment:

The journey from raw materials to the final Alloy 20 product involves intricate fabrication techniques and carefully orchestrated heat treatments. We dissect the fabrication process, highlighting the steps that shape Alloy 20 into its final form.Furthermore, we investigate the impact of heat treatment in improving the mechanical characteristics of the alloy and ensuring that it fits the requirements of diverse applications.

It is possible to cold-work or hot-work alloy 20 using conventional techniques. Prior to forging, hot forged material should be heated to a temperature between 2100°F and 2250°F with rigorous temperature management to ensure that the material does not drop below 1800°F. After hot working, anneal the material by raising its temperature to between 1725°F and 1850°F for at least 30 minutes per inch of thickness, and then quench it in water.

When stress relief is sought, heat to a temperature below 1000°F and then quench with water once the appropriate time has passed at the temperature. Alloy 20 should be annealed at a temperature of 1725°F to 1850°F for 30 minutes per inch of thickness. By heating to 2100°F, a reduced hardness can be achieved, although this may not be good for the alloy’s ability to stabilize.

Alloy 20 is often welded using TIG, MIG, and submerged arc welding (SAW), with the appropriate filler metal (ER320LR for TIG, MIG, and SAW, and E320LR for SAW). When welding to higher-grade alloys like C276 and Alloy 22, or to dissimilar alloys like 316, AWS ERNiCrMo-3 may be used for TIG and MIG, whereas ENiCrMo-3 can be used for SAW.

Other Designations – Equivalent:

  • ASME SB-462 – SB-464
  • ASME SB-468
  • ASTM B 462 – B 464
  • ASTM B 468
  • ASTM B 472 – B 474
  • ASTM B 751
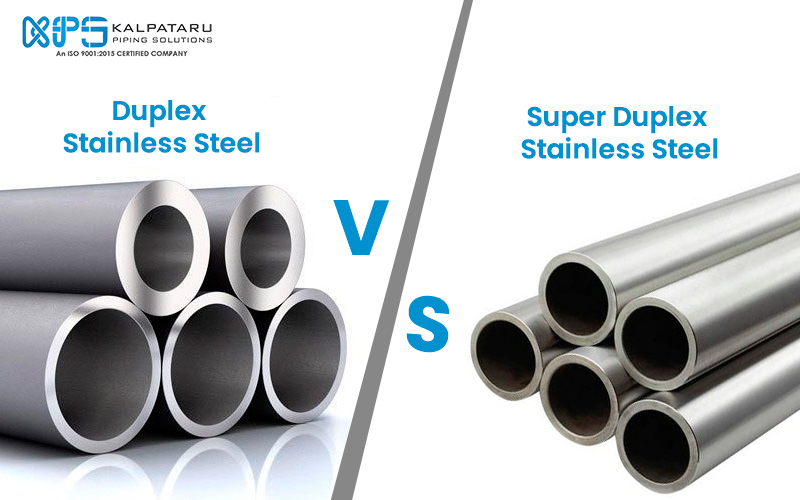
Difference Between Duplex and Super Duplex Stainless Steel

Difference Between Duplex and Super Duplex Stainless Steel

What is the Difference Between Duplex and Super Duplex Stainless Steel?

Significant difference between Super Duplex Stainless Steel and Duplex Stainless Steel. Super Duplex variants are characterized by a higher alloying addition of 25% chromium, in contrast to Duplex Stainless Steels with 22% chromium. Elevating the chromium content enhances the resistance to pitting corrosion. It’s important to note that these factors are not the sole determinants; other variables also play a role.

Duplex and Super duplex stainless steels are unique in that they feature both ferritic and austenitic phases within their metallurgic microstructure. This dual-phase structure allows them to exhibit the beneficial properties of both ferritic and austenitic stainless steels. The key components of these alloys include chromium, nickel, and molybdenum, with additional elements present in smaller quantities.

There are several key differences between duplex stainless steels and super duplex stainless steels. One of the main differences lies in their chromium content. Duplex stainless steels are typically composed of around 22% chromium, while super duplex stainless steels contain about 25% chromium. This increase in chromium content significantly enhances the pitting corrosion resistance of super duplex steels, making them more suitable for highly corrosive environments.

Price Difference Between Duplex and Super Duplex Stainless Steel

Super duplex materials, owing to their higher chromium, nickel, and molybdenum content, are more expensive compared to the standard duplex grades. Within both standard duplex and super duplex categories, various grades exist, each with its distinct material composition. As a result, the prices differ based on these compositions. Generally, a super duplex is pricier than the standard duplex grades due to its enhanced alloy content and superior properties.

What is Duplex Stainless Steel?

Duplex Stainless Steel is named for its dual-phase metallurgical structure, which includes both austenitic (face-centered cubic lattice) and ferritic (body-centered cubic lattice) phases. Unlike traditional austenitic stainless steels, duplex stainless steels have a higher chromium content (20-28%), up to 5% molybdenum, lower nickel content (around 9%), and a small amount of nitrogen (0.05-0.5%). This unique composition provides superior strength, corrosion resistance, and stress corrosion cracking resistance compared to standard austenitic stainless steels.

What is Super Duplex Stainless Steel?

The Pitting Resistance Equivalent Number (PREN) is calculated using the formula: PREN = %Cr + 3.3 x %Mo + 16 x %N, where Cr stands for chromium, Mo for molybdenum, and N for nitrogen. Increasing the chromium content boosts the PREN from 34 to over 40, which signifies enhanced resistance to pitting corrosion across various environments. Super duplex grades are the preferred choice for subsea and marine applications because of their proven durability in seawater.

Welding Duplex And Super Duplex Stainless Steel

One of the significant challenges when welding metallic components involves dealing with chromium carbide precipitation. This phenomenon can lead to intergranular corrosion and localized corrosion over the long term. Because both duplex and super duplex stainless steel include a high chromium concentration, they are susceptible to chromium carbide precipitation.

However, the extent of carbide precipitation is also influenced by the carbon content present in these materials. To mitigate this issue, proper preheating prior to welding is essential, followed by post-weld heat treatment. Fortunately, due to their inherent resistance to corrosion, both these materials are viable for welding, provided that the appropriate procedures are meticulously followed, and the correct parameters are diligently maintained.

Unlike conventional austenitic stainless steel alloys, which are affected in their entirety during welding, duplex stainless steels mainly experience issues in the Heat-Affected Zone (HAZ). The key problems in the HAZ during welding include loss of toughness, post-weld cracking, and reduced corrosion resistance. To address these challenges, experienced welders are needed to weld duplex grades using techniques like SAW (Submerged Arc Welding), TIG (Tungsten Inert Gas welding), and MIG (Metal Inert Gas welding). Additionally, proper post-welding processing is essential to maintain the integrity and properties of the alloys.

Strength Super Duplex Stainless Steel

Duplex stainless steel ranks high in strength compared to other stainless steels. It can bear a substantial amount of weight and withstand significant physical stress.

However, super duplex stainless steel offers even greater strength. For use in high-stress, high-impact environments, super duplex is the superior choice.

Duplex And Super Duplex Corrosion Resistance

As previously said, integrating chromium, nickel, molybdenum, nitrogen, and tungsten into their alloys improves their corrosion resistance. Pitting resistance can reach amazing values of up to 45. Furthermore, these alloys may be used at high temperatures without oxidation damage. They are also extremely resistant to different alkaline, acidic, and neutral solutions.

Duplex & Super Duplex Stainless Steel Cutting Speed

Cutting through duplex and super duplex stainless steel can be a challenge, but fear not! We’ve got you covered. Achieving the perfect cutting speed is crucial for efficient machining.

Duplex grades can be cut and machined faster than super duplex due to their composition. Super duplex, with its higher chromium, nickel, and molybdenum content, demands more precision and patience.

To tackle these materials like a pro, you’ll need top-notch tools and a slower cutting pace. Luckily, there are tests like the turning, chip formation, and drilling tests to help determine the ideal cutting speeds for various grades.

With the right approach, you’ll be cutting through duplex and super duplex stainless steel like a hot knife through butter!

Super Duplex Stainless Steel 2507

Super Duplex SS 2507 is a highly durable stainless steel alloy known for its exceptional strength and corrosion resistance. It has a dual-phase microstructure consisting of both austenite and ferrite, which provides superior mechanical properties compared to regular duplex and austenitic stainless steels. With high chromium (around 25%), molybdenum (around 4%), and nickel (around 7%) content, SS 2507 is particularly resistant to pitting, crevice corrosion, and chloride stress corrosion cracking. This makes it ideal for demanding applications in harsh environments, such as offshore oil and gas platforms, chemical processing, and marine industries.

Kalpataru Piping Solutions is a manufacturer and supplier of Duplex 2207 in a variety of shapes, sizes and more.

Duplex Stainless Steel Chemical Composition

Grade C Mn Si P S Cr Mo Ni N Fe
S31803 0.030 max 2.00 max 1.00 max 0.030 max 0.020 max 22.0 – 23.0 3.0 – 3.5 4.50 – 6.50 0.14 – 0.20 63.72 min
S32205 0.030 max 2.00 max 1.00 max 0.030 max 0.020 max 21.0 – 23.0 2.50 – 3.50 4.50 – 6.50 0.8 – 0.20 63.54 min

2205 Duplex Stainless Steel Equivalent

S31803 / S32205 Density Melting Point Yield Strength (0.2%Offset) Tensile Strength Elongation
7.8 g/cm3 1350 °C (2460 °F) Psi – 80000 , MPa – 550 Psi – 116000 , MPa – 800 15 %

Mechanical Properties of UNS S31803 Duplex 2205

STANDARD WERKSTOFF NR. UNS
Duplex 2205 1.4462 S31803 / S32205

Super Duplex SS 2507 Equivalent

Grade UNS EN W-Nr DIN AFNOR SS
Duplex 2707 HD Bars S32707
Duplex 2507 Bars S32750 1.4410 X 2 CrNiMoN 25 7 4 2328

Super Duplex 2507 Chemical Composition

C Si Mn P S Cr Ni Mo N Cu
≤0.030 ≤0.8 ≤1.2 ≤0.035 ≤0.015 25 7 4 0.3 ≤0.5

Mechanical Properties of Super Duplex UNS S32750

Proof strength Tensile strength Elong. Hardness
Rp0.2a) Rm Ab) Rockwell C
ksi ksi %
≥80 110-135 ≥25 ≤28

In conclusion, both duplex and super duplex steel offer significant advantages in various applications due to their excellent corrosion resistance, high strength, and durability. Duplex steel is ideal for environments where moderate to high corrosion resistance is required, offering a cost-effective solution with good mechanical properties. Super duplex steel, on the other hand, is suited for more demanding applications with higher levels of chloride and aggressive environments, providing enhanced performance and longer service life.

When choosing between duplex and super duplex steel, it’s crucial to consider the specific requirements of your project, including the environmental conditions, mechanical stress, and desired longevity. Both types of steel are exceptional choices, but the right selection will depend on the balance of cost, performance, and the specific demands of the application.

For more detailed information on our range of products, please visit our Duplex Steel and Super Duplex Steel product pages. These pages provide comprehensive insights into the specifications, applications, and benefits of each type of steel, helping you make an informed decision for your next project.To Know More About Our Product Click Here

Our Product

Hastelloy C276: Chemical Composition, Mechanical Properties

Hastelloy C276: Chemical Composition, Mechanical Properties

Hastelloy C276 (UNS N10276 / DIN 2.4819) is the most widely specified nickel-molybdenum-chromium alloy in severe corrosion service. Developed specifically to resist the broadest possible range of aggressive chemical environments, from strongly reducing acids to moderately oxidising media, Hastelloy C276 remains the benchmark corrosion-resistant alloy for chemical processing, oil and gas, flue gas desulfurisation (FGD), and pharmaceutical applications worldwide. Its exceptionally low carbon and silicon content minimises grain boundary precipitation during welding, enabling use in the as-welded condition without post-weld heat treatment in most service environments. Browse our complete Hastelloy Products range to explore all available product forms. 

Hastelloy C276 Chemical Composition (UNS N10276 / ASTM B622)

Hastelloy C276 chemical composition is defined under ASTM B622, B619, and B626. The alloy derives its outstanding corrosion resistance from a combination of high molybdenum (15–17 wt%), chromium (14.5–16.5 wt%), and tungsten (3–4.5 wt%), with nickel as the primary matrix element. Carbon is controlled to a maximum of 0.01 wt%, one of the tightest carbon limits of any commercial nickel alloy to suppress sensitisation and intergranular attack in the heat-affected zone of welds.

Element Min (wt%) Max (wt%) Nominal (wt%) Role Significance
Nickel (Ni) 57.0 Balance ~57% Matrix Base element; non-magnetic
Molybdenum (Mo) 15.0 17.0 16% Primary corrosion Reducing acid resistance, pitting
Chromium (Cr) 14.5 16.5 15.5% Oxidation Oxidising acid and high-temp resistance
Iron (Fe) 4.0 7.0 5.5% Diluent Cost reduction; minor effect
Tungsten (W) 3.0 4.5 3.75% Solid solution Enhances reducing acid resistance
Cobalt (Co) 2.5 max Trace Controlled impurity
Carbon (C) 0.01 max Weld control Ultra-low; prevents sensitisation
Manganese (Mn) 1.0 max Impurity Controlled for cleanliness
Silicon (Si) 0.08 max Weld control Low Si = better weld ductility
Vanadium (V) 0.35 max Trace Impurity limit
Phosphorus (P) 0.04 max Impurity Low for weld quality
Sulphur (S) 0.03 max Impurity Controlled for hot workability

Hastelloy C276 Physical Properties

The following physical properties apply to Hastelloy C276 (UNS N10276) in the solution-annealed condition at room temperature.

Property Value Unit / Notes
Density 8.89 g/cm³ (0.321 lb/in³)
Melting Range 1325 – 1370 °C (2415–2500°F)
Specific Heat 427 J/kg·°C at 20°C
Thermal Conductivity 10.2 W/m·°C at 20°C
Electrical Resistivity 1.30 µΩ·m at 20°C
Modulus of Elasticity 205 GPa (29.7 × 10⁶ psi)
Magnetic Permeability 1.0004 Essentially non-magnetic
Coefficient of Thermal Expansion 11.2 µm/m·°C (20–100°C)

Hastelloy C276 Mechanical Properties: Solution Annealed Condition

Hastelloy C276 tensile strength and other mechanical properties in the solution-annealed condition meet the minimum requirements of ASTM B622 (sheet/plate/strip), B619 (welded pipe), and B626 (welded tube). Properties shown are minimum specification values; individual heats typically exceed these on the Material Test Report (MTR).

Property Metric (SI) Imperial ASTM Minimum
Ultimate Tensile Strength (UTS) 690 MPa 100 ksi 690 MPa
0.2% Proof Strength (Yield) 283 MPa 41 ksi 283 MPa
Elongation (in 50 mm) 40% 40% 40% min
Hardness (Rockwell B) 100 HRB max 100 HRB max 100 HRB
Hardness (Brinell) 241 HB max 241 HB max
Impact Strength (Charpy V) >100 J >74 ft·lbf

Unlike precipitation-hardened nickel alloys such as Inconel 718, Hastelloy C276 achieves its strength entirely through solid-solution strengthening. There is no aging heat treatment requirement, simplifying procurement, fabrication, and quality assurance. 

Hastelloy C276 Corrosion Resistance

Hastelloy C276 corrosion resistance is the defining characteristic of this alloy and the primary reason for its specification across chemical processing, oil and gas, and environmental engineering applications. The combination of high molybdenum and tungsten provides outstanding resistance in reducing environments, while chromium provides adequate performance in moderately oxidising conditions. 

Hydrochloric Acid (HCl)

Hastelloy C276 hydrochloric acid resistance is exceptional. The alloy resists all concentrations of HCl at temperatures up to approximately 40°C and dilute concentrations (below 2%) up to boiling point. This is the single most demanding test environment for any corrosion-resistant alloy, and C276 outperforms all grades of stainless steel and most nickel alloys in this medium. ISO-corrosion diagrams show C276 performing well where 316L stainless steel shows corrosion rates exceeding 1.0 mm/year. 

Sulfuric Acid (H₂SO₄)

Hastelloy C276 sulfuric acid resistance covers the full concentration range from dilute to concentrated H₂SO₄ at ambient conditions, and a wide range of concentrations at elevated temperatures. The alloy is particularly valuable in mixed acid streams where H₂SO₄ is combined with oxidising contaminants (e.g., ferric chloride or cupric chloride) that would attack pure reducing-resistant alloys. 

Oxidising and Reducing Mixed Environments

One of the most significant advantages of Hastelloy C276 over many speciality alloys is its ability to tolerate swings between oxidising and reducing conditions within the same process stream. Chemical plant upsets, process changeovers, and mixed-acid streams often expose piping and vessels to both regimes simultaneously. C276 provides a reliable safety margin in these unpredictable environments. 

Key Corrosive Environments Where C276 is Specified

  • Hydrochloric acid (HCl) — all concentrations below 40°C; dilute HCl to boiling
  • Sulfuric acid (H₂SO₄) — wide concentration range; superior to Inconel 625 in hot dilute H₂SO₄
  • Wet chlorine gas — excellent; resists chlorine and hypochlorite below ~70°C
  • Ferric chloride (FeCl₃) and cupric chloride (CuCl₂) — oxidising chloride pitting solutions
  • Phosphoric acid — good resistance across concentrations to boiling
  • Acetic, formic, and other organic acids — excellent across a broad range
  • Seawater and saline solutions — high PREN; resistant to crevice and pitting attack
  • Sour gas (H₂S + CO₂ + Cl⁻) — NACE MR0175 / ISO 15156 compliant
  • Flue gas condensate — FGD scrubber service with SO₂, HCl, and HF in solution

Note: Hastelloy C276 is NOT recommended for concentrated nitric acid, fuming nitric acid, or strongly oxidising media at elevated temperatures  for those environments, specify Hastelloy C-22 or Hastelloy C-2000. 

Hastelloy C276 vs C22  Comparison

The Hastelloy C276 vs C22 comparison is the most frequently asked question in corrosion-resistant alloy selection. Both alloys are based on the Ni-Cr-Mo system; the key difference lies in the oxidising-to-reducing balance of the service environment.

Property / Environment Hastelloy C276 Hastelloy C22
UNS Number N10276 N06022
Chromium % 14.5–16.5 20.0–22.5 (higher)
Molybdenum % 15.0–17.0 12.5–14.5 (lower)
Tungsten % 3.0–4.5 2.5–3.5
Reducing Acid Resistance Excellent — primary strength (high Mo + W) Very Good
Oxidising Acid Resistance Good Excellent — primary strength (high Cr)
Mixed Acid Environments Excellent Excellent — slightly broader oxidising range
HCl Resistance Superior Very Good
Concentrated HNO₃ Resistance Limited — not recommended Good
Weldability Excellent; no PWHT required Excellent; no PWHT required
ASTM Specifications B622 / B619 / B626 / B574 B622 / B619 / B626 / B574
Typical Application Reducing & mixed chemical environments, HCl-bearing streams Oxidising + reducing environments, waste treatment, mixed acids
Select When… Process is predominantly reducing with chloride exposure Process has significant oxidising component (HNO₃, Cl₂, FeCl₃) or alternating regimes

Hastelloy C276 vs Inconel 625  Comparison

The Hastelloy C276 vs Inconel 625 selection question frequently arises in offshore, chemical, and FGD applications, where both alloys are commonly available and specified. The decision turns on temperature range, fabrication complexity, and the specific corrosive media involved.

Property Hastelloy C276 (N10276) Inconel 625 (N06625)
Primary Alloying Ni-Mo-Cr-W (Mo 16%, Cr 15.5%) Ni-Cr-Mo-Nb (Mo 9%, Cr 21%, Nb 3.6%)
Corrosion Focus Reducing & mixed acid chemical service Broad corrosion + high temperature structural
HCl Resistance Superior (Mo 16%) Good (Mo 9%)
H₂SO₄ Resistance Excellent — hot dilute H₂SO₄ Good
Pitting Resistance (PREN) ~70 (very high) ~51 (high)
Max Service Temperature 1038°C (1900°F) — oxidation 982°C (1800°F) — Gr.1 / 593°C Gr.2 creep
High-Temp Structural Strength Moderate Superior (Nb solid solution hardening)
Weldability / PWHT Excellent; no PWHT required Excellent; no PWHT required
Cost Typically higher (higher Mo content) Lower — more widely stocked
Select When… Severe reducing acid / mixed chemical environments dominate Offshore, subsea, high-temp service, or where fabrication cost matters

Hastelloy C276 Temperature Resistance and Performance

Hastelloy C276 temperature resistance covers a broad service range. In aqueous corrosion service, the alloy performs from cryogenic temperatures (below -196°C with appropriate impact testing) up to approximately 400°C before specific corrosion resistance begins to diminish in certain media. At elevated temperature in air or combustion atmospheres, oxidation resistance extends to 1038°C (1900°F).

  • Cryogenic service: Suitable with impact testing to -196°C
  • Ambient to 400°C: Full corrosion resistance in most specified media
  • 400°C – 650°C: Elevated temperature use generally limited to non-corrosive or mildly corrosive environments; consult NACE guidelines for sour gas service
  • Above 650°C to 1038°C: Oxidation resistance in air; suitable for furnace components, catalyst support hardware
  • ASME Boiler & Pressure Vessel Code (ASME B31.3 / ASME Section VIII) allowable stress values available up to 815°C

Important note: Hastelloy C276 should not be exposed to temperatures between 540–760°C for extended periods in service — this range promotes precipitation of intermetallic phases (mu-phase and sigma-phase) that can reduce toughness and ductility. 

Hastelloy C276 Weldability and Fabrication

Hastelloy C276 weldability is one of the alloy’s most commercially important properties. The ultra-low carbon (0.01% max) and silicon (0.08% max) content minimises carbide and silicide precipitation in the weld heat-affected zone, allowing the alloy to be used in the as-welded condition for most service environments without requiring post-weld solution annealing. 

Welding Processes

  • GTAW (TIG) — preferred for root passes and thin-wall pipe; use ERNiCrMo-4 filler (AWS specification) which matches C276 nominal chemistry
  • GMAW (MIG) — suitable for thicker sections
  • SMAW — E NiCrMo-4 covered electrode
  • SAW (submerged arc) — not generally recommended; can dilute alloy content

Fabrication Notes

  • Solution anneal after severe cold working: 1121°C (2050°F) minimum, water quench
  • Machining: moderate difficulty — work hardening rate is significant; use sharp tooling, positive rake angles, and adequate coolant flow; reduce cutting speeds vs 316L stainless by approximately 30%
  • Forming: Cold forming is feasible with standard tooling; allow for springback; solution anneal if >15% cold reduction
  • Avoid contamination with iron particles — clean all tooling and contact surfaces before fabrication

Hastelloy C276 machinability: CNC turning and milling are standard. Work hardening requires lower feed rates, higher cutting speeds, and more frequent tool changes than 316L stainless steel. Flood coolant is mandatory. For drilling, use stub-length drills to minimise deflection. Estimated machining cost premium vs 316L stainless: 2–3×. 

Hastelloy C276 Industry Applications

Hastelloy C276 applications span every major process industry segment where corrosive chemicals are handled at elevated temperatures or pressures:

Chemical Processing

  • Reactors, columns, and heat exchangers handling HCl, H₂SO₄, phosphoric acid, and mixed-acid streams
  • Chlorinated solvent production — vinyl chloride, methylene chloride, chlorobenzene
  • Acid concentration plants and acid recovery systems
  • Pickling and etching equipment

Oil and Gas — Upstream and Downstream

  • Sour gas (H₂S + CO₂ + Cl⁻) wellhead equipment, tubing hangers, and Christmas tree components
  • Downhole completion tools in high-chloride, high-CO₂ wells
  • Process vessels and heat exchangers handling crude containing naphthenic acid
  • FPSO topside piping in aggressive seawater service

Flue Gas Desulfurisation (FGD)

Hastelloy C276 FGD applications represent one of the highest-volume uses of the alloy. Coal-fired and industrial plant scrubbers handle wet flue gas containing dissolved SO₂, HCl, HF, and fly ash particulates at temperatures of 50–80°C — a uniquely aggressive mixed-acid environment that eliminates rubber-lined carbon steel, fibreglass, and most stainless grades. C276 provides long-term service life for absorber vessels, ducts, spray lances, and mist eliminators.

Pulp and Paper

  • Chlorine dioxide bleaching circuits — digester and bleach plant equipment
  • White liquor and green liquor handling systems
  • Evaporator tubes in the black liquor circuit

Pharmaceutical and Fine Chemical

  • Reactor vessels, agitators, and pipework in multi-purpose API manufacturing plants
  • USP-grade process piping where cross-contamination prevention is required
  • Highly corrosive intermediates and specialty chemical synthesis

Marine and Environmental

  • Seawater handling and desalination components
  • Offshore platform systems in aggressive splash zone environments
  • Industrial and municipal wastewater treatment, scrubbers, oxidation vessels

Hastelloy C276 Available Product Forms

Kalpataru Piping supplies the complete range of Hastelloy C276 product forms in accordance with ASTM B622 (sheet/plate/strip), B619 (welded pipe), B626 (welded tube), and B574 (bar). All products are supplied with certified Material Test Reports (MTRs), and third-party inspection is available on request:

Conclusion

Hastelloy C276 (UNS N10276 / DIN 2.4819) remains the benchmark nickel alloy for severe chemical corrosion service after more than five decades of industrial use. Its combination of high molybdenum, chromium, and tungsten content  together with ultra-low carbon and silicon delivers reliable, long-service performance in the most aggressive reducing, mixed-acid, and chloride-bearing environments encountered in chemical, oil and gas, FGD, pulp and paper, and pharmaceutical applications. 

When evaluating Hastelloy C276 against Hastelloy C-22 or Inconel 625: C276 is the choice for predominantly reducing and HCl-dominated environments; C-22 is the step-up when significant oxidising acids (HNO₃, wet Cl₂) are also present; Inconel 625 is the more economical selection for offshore and high-temperature structural applications where its Nb content and ASTM B444 seamless tube availability are advantageous.

View all Nickel Alloy Products supplied by Kalpataru Piping, or submit your project specification for a technical review and quotation.

Enquire Now
close slider

    Enquire Now

    Fill the below form and get in touch with us, we’ll call you back.

    Fill the Captcha:
    WhatsApp chat